GST : 24AACCI2791M1ZB

call images

Call us

08045478223

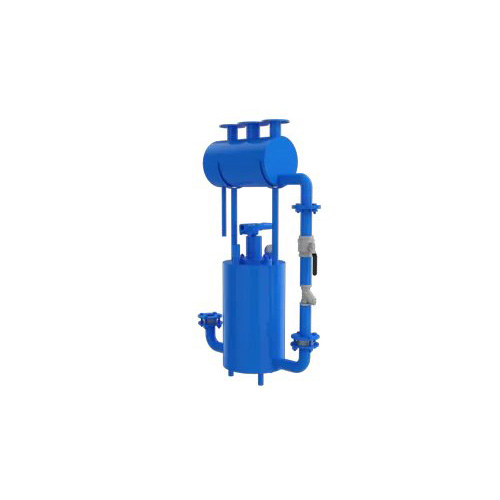
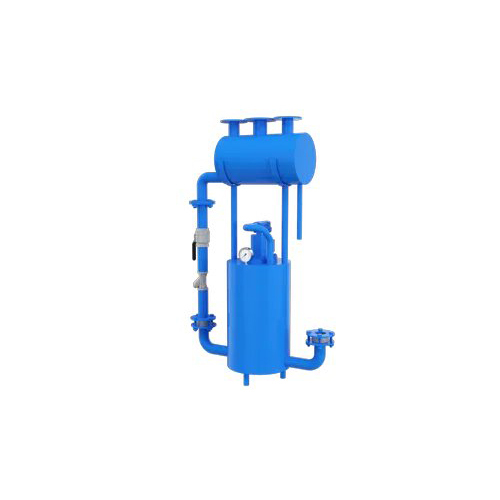
Steam Condensate Return Pump

Steam Condensate Return Pump

Price 100000 INR/ Unit

MOQ : 1 Unit

Steam Condensate Return Pump Specification

  • Flow Rate
  • Up to 12 m/h
  • Frequency
  • 50 Hz / 60 Hz
  • Theory
  • Centrifugal Pump / Mechanical Condensate Recovery
  • Mounting Type
  • Base-mounted / Skid-mounted
  • Speed
  • 1450 rpm / 2900 rpm
  • Head Size
  • Up to 40 m
  • Max Suction
  • 6 m
  • Features
  • Corrosion-resistant, Low maintenance, High reliability
  • Noise Level
  • Below 60 dB(A)
  • Control System
  • Float switch / Automatic Level Control
  • Discharge Pressure
  • 1-5 bar
  • Voltage
  • 220V / 380V / 415V, 3 Phase
  • Working Temperature
  • Up to 120C
  • Inlet/Outlet
  • DN25 to DN80
  • Caliber
  • 25 mm to 80 mm
  • Material
  • Cast Iron / Stainless Steel
  • Structure
  • Horizontal single-stage
  • Power
  • 0.75 kW to 5.5 kW
  • Standard
  • IS / ISO / DIN
  • Fuel Type
  • Electric
  • Pressure
  • Up to 5 bar
  • Usage
  • Other
  • Application
  • Other
  • Suction Type
  • Side or End Suction
  • Seals Type
  • Mechanical Seal
  • Priming
  • Self-priming
  • Pump Type
  • Condensate Transfer Pump
  • Capacity
  • Upto 500 LPM
  • Overflow Provision
  • Integrated overflow
  • Min Liquid Temperature
  • 15C
  • Tank Material
  • Mild Steel / SS304 for receiver tank
  • Safety Feature
  • Thermal overload protection
  • Return Connection
  • Threaded / Flanged
  • Vibration Level
  • < 1.8 mm/s
  • Impeller Type
  • Closed / Semi-open impeller
  • Insulation Class
  • F / H
  • Max Working Pressure
  • 5 bar
  • Ambient Temperature
  • Up to 50C
  • Accessories Available
  • Non-return valve, Sight glass, Level controller
  • Pump Casing Pressure
  • Tested up to 10 bar
  • Protection Class
  • IP55 / IP65
  • Cooling Method
  • Air-cooled motor
  • Service Life
  • Designed for 25,000 hours
 

Steam Condensate Return Pump Trade Information

  • Minimum Order Quantity
  • 1 Unit
  • Supply Ability
  • 100 Units Per Month
  • Delivery Time
  • 1 Week
 

About Steam Condensate Return Pump


Introducing our Steam Condensate Return Pump, a cornerstone of efficiency in industrial steam systems. This pump excels in reclaiming and returning condensate to the boiler, preventing energy wastage and optimizing overall system performance. Crafted for reliability and durability, it operates seamlessly in diverse industrial environments. The user-friendly design ensures easy integration into existing setups, providing a hassle-free solution for condensate management. By recovering and recycling condensate effectively, this pump not only trims operational costs but also aligns with sustainability goals, minimizing environmental impact. Elevate your steam system's efficiency with our Steam Condensate Return Pump a dependable, cost-effective, and environmentally conscious solution for fluid management. 

Specification

Max Flow Rate

1 to 12 TPH

Model Name/Number

IEPL CONDENSATE ERECOVERY PUMP

Brand

Innovative Enerpro Pvt Ltd.

Color

Blue

Material

S.S, M.S

Country of Origin

Made in India


High-Endurance Construction and Safety

This pump is engineered for prolonged service life with a 25,000-hour design and robust mild steel or SS304 receiver tank. It includes key safety features such as thermal overload protection, integrated overflow provision, and operates effectively in ambient temperatures up to 50C. With insulation class F/H and IP55/IP65 protection, it is suitable for demanding industrial environments.


Efficiency and Versatility for Industrial Applications

Thanks to its air-cooled, self-priming motor and centrifugal design, the pump supports a vast array of applications. It operates reliably at working temperatures up to 120C, with flow rates up to 12 m3/h and suction lifts up to 6 meters. Built for versatility, it accommodates DN25 to DN80 connections and is available with automatic level control accessories.

FAQ's of Steam Condensate Return Pump:


Q: How does the Steam Condensate Return Pump improve condensate recovery in industrial boiler systems?

A: The pump facilitates the automatic transfer of hot condensate from process equipment back to the boiler, significantly reducing water and fuel consumption by recycling usable condensate. This mechanism helps maintain boiler efficiency and minimizes energy loss, benefiting both operational costs and sustainability goals.

Q: What types of impellers and casing materials are available for this pump?

A: The pump is available with closed or semi-open impellers, catering to varied liquid qualities and operating conditions. Pump casing and receiver tank materials include robust cast iron or corrosion-resistant stainless steel (SS304), ensuring compatibility with a broad range of industrial applications and condensate conditions.

Q: When should the integrated thermal overload protection be relied upon?

A: Thermal overload protection activates automatically during excessive load or overheating, helping to prevent motor damage. Users can rely on this safety feature during unpredictable operating conditions or voltage fluctuations to ensure uninterrupted service and extended pump lifespan.

Q: Where can this pump be installed and what mounting options are offered?

A: The pump is suitable for steam condensate return systems in power plants, HVAC facilities, and industrial boiler houses. It can be installed on a base-mounted or skid-mounted setup, providing flexibility for new or retrofit installations according to site requirements.

Q: What is the process for maintaining low vibration and noise levels during pump operation?

A: Designed to operate below 1.8 mm/s vibration and under 60 dB(A) noise level, the pump incorporates precision balancing, high-quality bearings, and a robust enclosure. Routine inspection and timely maintenance of mechanical seals and bearings are recommended to sustain optimal low-noise, low-vibration performance.

Q: What are the key usage benefits of this condensate return pump in industrial environments?

A: This pump offers reliable condensate management, self-priming capability, and automatic level control, minimizing manual intervention. Its corrosion-resistant construction, integrated accessories such as sight glass and non-return valve, and compliance with IS/ISO/DIN standards ensure high performance, low maintenance, and long-term operational safety.

Tell us about your requirement
product

Price:

Quantity
Select Unit

  • 50
  • 100
  • 200
  • 250
  • 500
  • 1000+
Additional detail
Mobile number

Email

More Products in Condensate Recovery System Category

Condensate Recovery Pump

Condensate Recovery Pump

Price 100000 INR / Unit

Minimum Order Quantity : 1 Unit

Flow Rate : 1 to 10 m/hr

Material : Cast Iron / Stainless Steel

Priming : SelfPriming / NonSelfPriming

Frequency : 50 Hz
Pressure Powered Pumping Packaged Unit

Pressure Powered Pumping Packaged Unit

Price 150000 INR / Unit

Minimum Order Quantity : 1 Unit

Flow Rate : 0.5 m/h to 10 m/h

Material : Cast Iron / SS304 / SS316

Priming : Selfpriming

Frequency : 50 Hz / 60 Hz
Condensate Pump

Condensate Pump

Price 120000 INR / Unit

Minimum Order Quantity : 1 Unit

Flow Rate : 24 liters/hour

Material : ABS Plastic

Priming : Selfpriming

Frequency : 50Hz
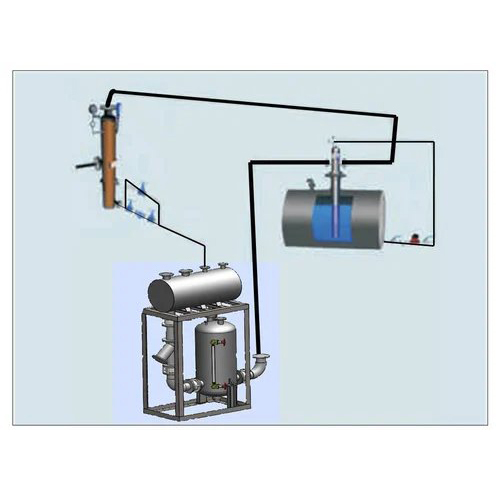
Steam Condensate Return System

Steam Condensate Return System

Price 160000 INR / Unit

Minimum Order Quantity : 1 Unit

Flow Rate : 0.5 m/hr to 20 m/hr

Material : Mild Steel / Stainless Steel (SS304, SS316)

Priming : Self / Manual Priming

Frequency : 50 Hz


Back to top